Corner radius end mills
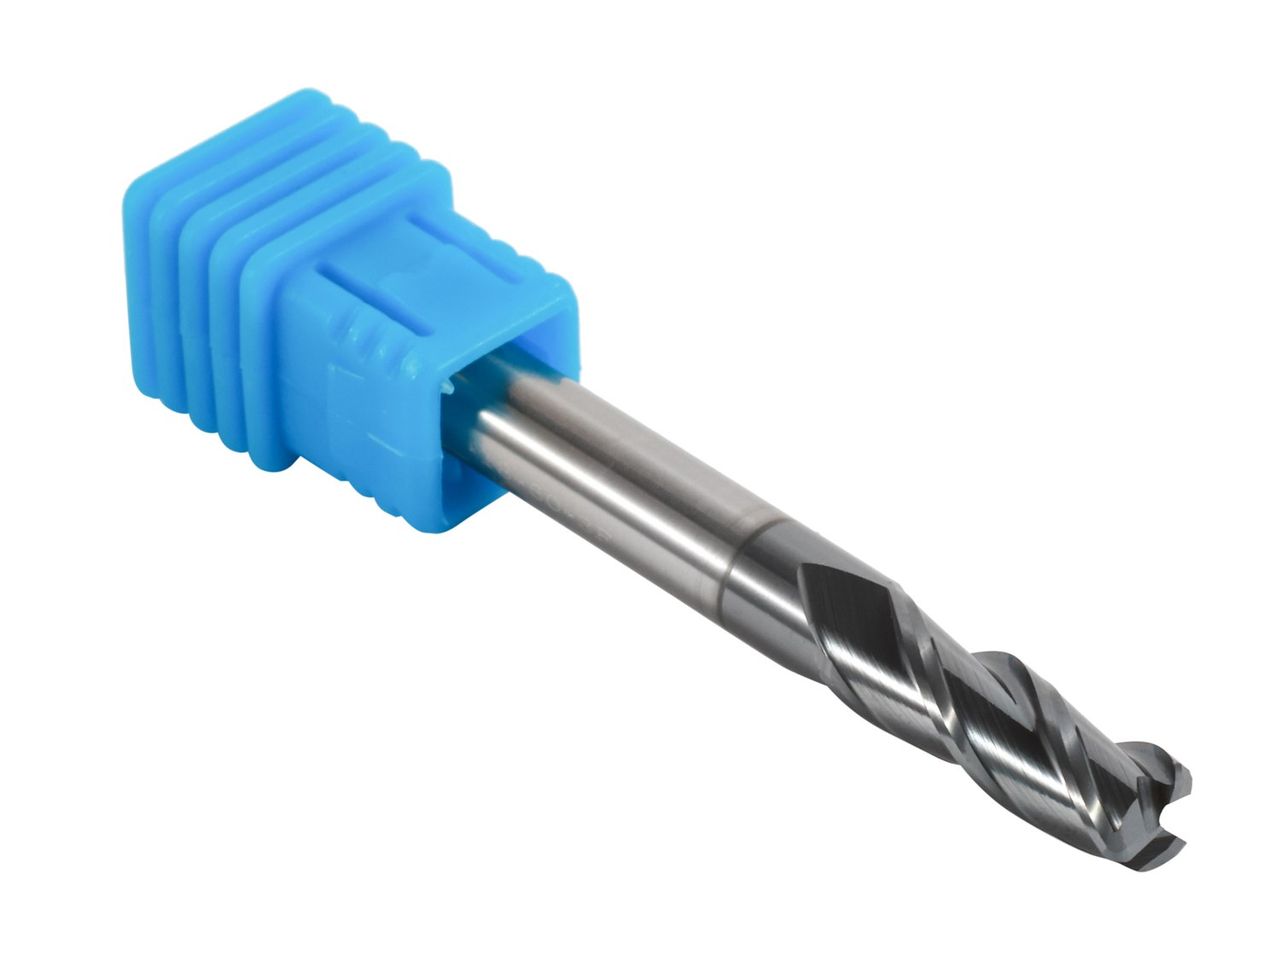
Solid carbide corner radius end mills for steel. A radius on the corner instead of a sharp edge strengthens the cutting corner and leaves a radius where the floor meets the wall. The HRC55, HRC58 and HRC60 series cover Φ1 to Φ20 mm with corner radii from R0.2 to R3.
Choosing a corner radius
Start from the radius on the part drawing: the tool leaves that radius where the floor meets the wall. Where the drawing allows a choice, a larger radius makes the cutting corner stronger and less likely to chip, while a smaller radius keeps the transition tight. Then check the cutting length against the depth and choose the shortest tool the part allows.
Corner radius size tables
HRC55 Corner Radius End Mill for Steel
| Cutting diameter (mm) | Radius (mm) | Cutting length (mm) | Overall length (mm) | Shank (mm) |
|---|---|---|---|---|
| D1 | R0.2 | 3 | 50 | D4 |
| D1.5 | R0.2 | 3.8 | 50 | D4 |
| D2 | R0.2/R0.5 | 5 | 50 | D4 |
| D2.5 | R0.2/R0.5 | 6.25 | 50 | D4 |
| D3 | R0.2/R0.5 | 8 | 50 | D4 |
| D4 | R0.2/R0.5/R1 | 10 | 50 | D4 |
| D4 | R0.2/R0.5 | 12 | 75 | D4 |
| D4 | R0.2/R0.5/R1 | 16 | 100 | D4 |
| D6 | R0.2/R0.5/R1 | 15 | 50 | D6 |
| D6 | R0.2/R0.5/R1 | 18 | 75 | D6 |
| D6 | R0.2/R0.5/R1 | 24 | 100 | D6 |
| D8 | R0.2/R0.5/R1 | 20 | 60 | D8 |
| D8 | R0.2/R0.5/R1 | 24 | 75 | D8 |
| D8 | R0.2/R0.5/R1 | 32 | 100 | D8 |
| D10 | R0.2/R0.3/R0.5/R1/R2/R3 | 25 | 75 | D10 |
| D10 | R0.2/R0.5/R1/ R2 | 40 | 100 | D10 |
| D12 | R0.2/R0.5/R1/ R2 | 30 | 75 | D12 |
| D12 | R0.2/R0.5/R1/ R2 | 45 | 100 | D12 |
| D12 | R1 | 60 | 150 | D12 |
| D14 | R2 | 45 | 100 | D14 |
| D16 | R0.2/R0.5/R1/ R2/R3 | 45 | 100 | D16 |
HRC58 Corner Radius End Mill for Steel
| Cutting diameter (mm) | Radius (mm) | Cutting length (mm) | Overall length (mm) | Shank (mm) |
|---|---|---|---|---|
| D1.5 | R0.2 | 3.8 | 50 | D4 |
| D2 | R0.2 | 5 | 50 | D4 |
| D2.5 | R0.2 | 6.25 | 50 | D4 |
| D3 | R0.2/R0.5 | 8 | 50 | D4 |
| D4 | R0.5/R1 | 10 | 50 | D4 |
| D4 | R0.5/R1 | 12 | 75 | D4 |
| D4 | R0.5/R1 | 16 | 100 | D4 |
| D5 | R0.2/R0.5 | 13 | 50 | D6 |
| D6 | R0.2/R0.3/ R0.5/R1 | 15 | 50 | D6 |
| D6 | R0.5/R1 | 18 | 75 | D6 |
| D6 | R0.5/R1 | 24 | 100 | D6 |
| D8 | R0.2/R0.5/R1 | 20 | 60 | D8 |
| D8 | R0.5/R1 | 24 | 75 | D8 |
| D8 | R0.5/R1 | 32 | 100 | D8 |
| D10 | R0.5/R1 | 25 | 75 | D10 |
| D10 | R0.5/R1 | 40 | 100 | D10 |
| D12 | R0.5/R1 | 30 | 75 | D12 |
| D12 | R0.5/R1 | 45 | 100 | D12 |
| D16 | R0.5/R1 | 45 | 100 | D16 |
| D20 | R1 | 45 | 100 | D20 |
HRC60 Corner Radius End Mill for Steel
| Cutting diameter (mm) | Radius (mm) | Cutting length (mm) | Overall length (mm) | Shank (mm) |
|---|---|---|---|---|
| D2 | R0.5 | 5 | 50 | D4 |
| D3 | R0.5 | 8 | 50 | D4 |
| D4 | R0.5/R1 | 10 | 50 | D4 |
| D4 | R0.5/R1 | 12 | 75 | D4 |
| D4 | R0.5/R1 | 16 | 100 | D4 |
| D5 | R0.5 | 13 | 50 | D5 |
| D5 | R0.5 | 13 | 50 | D6 |
| D6 | R0.5/R1 | 15 | 50 | D6 |
| D6 | R0.5/R1 | 18 | 75 | D6 |
| D6 | R0.5/R1 | 24 | 100 | D6 |
| D8 | R0.2/R0.5/R1 | 20 | 60 | D8 |
| D8 | R0.5/R1 | 24 | 75 | D8 |
| D8 | R0.5/R1 | 32 | 100 | D8 |
| D10 | R0.5/R1 | 25 | 75 | D10 |
| D10 | R0.5/R1 | 40 | 100 | D10 |
| D12 | R0.5/R1 | 30 | 75 | D12 |
| D12 | R0.5/R1 | 45 | 100 | D12 |
When to choose another series
- Square corners? Solid carbide end mills →
- Full radius for 3D surfaces? Ball nose end mills →
- Machining aluminium? End mills for aluminium →
Questions about this range
Corner radius or ball nose end mill?
A corner radius end mill has a flat bottom with a small radius at each corner, for pockets and shoulders with a radiused floor edge. A ball nose end mill has a full radius, for 3D profiling and curved surfaces.
Which radii are listed?
The tables list the radius available for each diameter in the HRC55, HRC58 and HRC60 series. The number is the workpiece hardness (HRC) each series is made for.
Do you make other radii or diameters?
Yes, other corner radii, diameters and lengths are made to drawing.
Catalog pages for this range
- Catalog 2026 Supplement PDF · 16 pages · 2.0 MB
Edition: October 2026. Free to download, no sign-up. All catalog downloads →