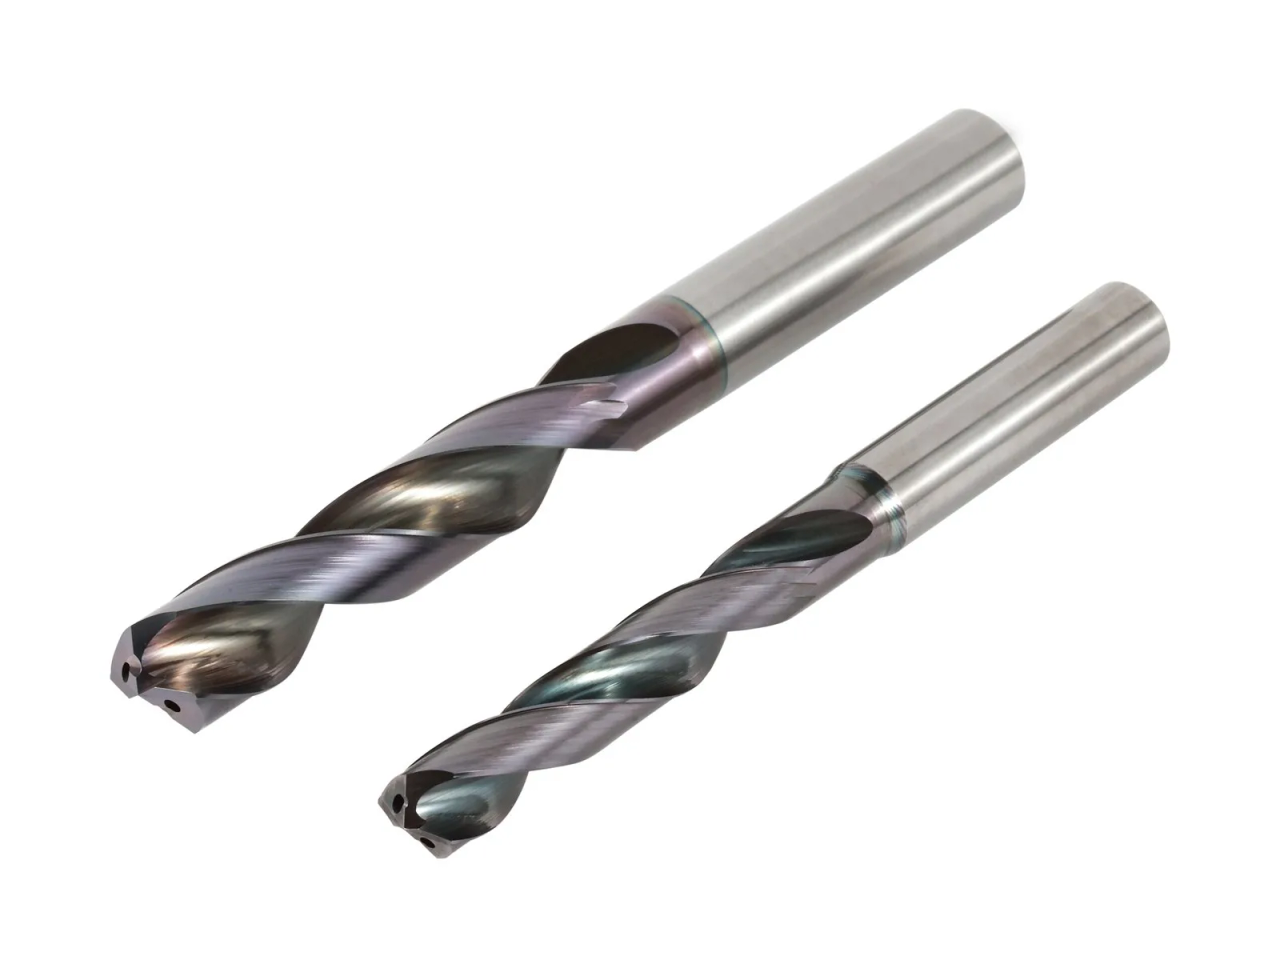
A tapped or thread-milled hole starts as a drilled hole. The drill sets the minor diameter of the thread, so it also sets how much material the tap or thread mill has to remove. Too small, and the tap is overloaded and may break. Too large, and the thread is shallow.
The tables below give the drill diameter for each thread and the pre-hole limits the drilled hole should fall within.
Jump to: Metric coarse · UNC · UNF · Metric fine
How to read the tables
- Drill is the standard drill diameter in our catalog for that thread.
- Hole limits are the catalog’s class 2 (6H for metric) limits for the drilled hole. Measure the hole before threading: it should fall between the two values.
- All values are in millimetres, including the inch threads. The catalog does not give inch, letter or number drill sizes, so they are not listed here.
- For metric coarse threads, the drill is close to the nominal diameter minus the pitch: M6×1 → 5, M8×1.25 → 6.8, M10×1.5 → 8.5.
- A few sizes from the catalog tables are not listed here. If you need one of them, ask us.
- These sizes are for cutting taps and thread mills. A forming tap needs a larger hole; for our solid carbide forming taps we give the hole size with the quote.
Source: DELEVEL Catalog 2026, chapter 07, p.156–158. Values as given in the catalog.
Metric coarse threads
| Thread | Drill, mm | Hole limits, mm |
|---|---|---|
| M1.0×0.25 | 0.75 | 0.729–0.785 |
| M1.1×0.25 | 0.85 | 0.829–0.885 |
| M1.2×0.25 | 0.95 | 0.929–0.985 |
| M1.4×0.3 | 1.1 | 1.075–1.142 |
| M1.6×0.35 | 1.25 | 1.221–1.321 |
| M1.7×0.35 | 1.35 | 1.321–1.421 |
| M1.8×0.35 | 1.45 | 1.421–1.521 |
| M2.0×0.4 | 1.6 | 1.567–1.679 |
| M2.2×0.45 | 1.75 | 1.713–1.838 |
| M2.3×0.4 | 1.9 | 1.867–1.979 |
| M2.5×0.45 | 2.1 | 2.013–2.138 |
| M2.6×0.45 | 2.2 | 2.113–2.238 |
| M3.0×0.5 | 2.5 | 2.459–2.599 |
| M3.5×0.6 | 2.9 | 2.85–3.01 |
| M4.0×0.7 | 3.3 | 3.242–3.422 |
| M4.5×0.75 | 3.8 | 3.688–3.878 |
| M5.0×0.8 | 4.2 | 4.134–4.334 |
| M6.0×1.0 | 5 | 4.917–5.153 |
| M7.0×1.0 | 6 | 5.917–6.153 |
| M8.0×1.25 | 6.8 | 6.647–6.912 |
| M9.0×1.25 | 7.8 | 7.647–7.912 |
| M10×1.5 | 8.5 | 8.376–8.676 |
| M11×1.5 | 9.5 | 9.376–9.676 |
| M12×1.75 | 10.3 | 10.106–10.441 |
| M14×2.0 | 12 | 11.835–12.21 |
| M16×2.0 | 14 | 13.835–14.21 |
| M18×2.5 | 15.5 | 15.294–15.744 |
| M20×2.5 | 17.5 | 17.294–17.744 |
| M22×2.5 | 19.5 | 19.294–19.744 |
| M24×3.0 | 21 | 20.752–21.252 |
| M27×3.0 | 24 | 23.752–24.252 |
| M30×3.5 | 26.5 | 26.211–26.771 |
UNC (unified coarse)
Nominal diameter in brackets, mm.
| Thread | Drill, mm | Hole limits, mm |
|---|---|---|
| No. 1-64 (1.854) | 1.55 | 1.425–1.582 |
| No. 2-56 (2.184) | 1.80 | 1.695–1.871 |
| No. 3-48 (2.515) | 2.10 | 1.941–2.146 |
| No. 4-40 (2.845) | 2.30 | 2.157–2.385 |
| No. 5-40 (3.175) | 2.60 | 2.487–2.697 |
| No. 6-32 (3.505) | 2.80 | 2.642–2.895 |
| No. 8-32 (4.166) | 3.40 | 3.302–3.53 |
| No. 10-24 (4.826) | 3.90 | 3.683–3.962 |
| No. 12-24 (5.486) | 4.50 | 4.344–4.597 |
| 1/4-20 | 5.10 | 4.979–5.257 |
| 5/16-18 | 6.60 | 6.401–6.731 |
| 3/8-16 | 8.00 | 7.798–8.153 |
| 7/16-14 | 9.40 | 9.144–9.55 |
| 1/2-13 | 10.80 | 10.592–11.023 |
| 9/16-12 | 12.20 | 11.989–12.446 |
| 5/8-11 | 13.60 | 13.386–13.868 |
| 3/4-10 | 16.50 | 16.307–16.840 |
| 7/8-9 | 19.50 | 19.177–19.761 |
| 1-8 | 22.20 | 21.971–22.606 |
| 1-1/8-7 | 25.00 | 24.638–25.349 |
| 1-1/4-7 | 28.20 | 27.813–28.524 |
| 1-3/8-6 | 30.80 | 30.353–31.115 |
| 1-1/2-6 | 34.00 | 33.528–34.290 |
| 1-3/4-5 | 39.50 | 38.964–39.827 |
| 2-4½ | 45.20 | 44.679–45.593 |
UNF (unified fine)
Nominal diameter in brackets, mm.
| Thread | Drill, mm | Hole limits, mm |
|---|---|---|
| No. 0-80 (1.524) | 1.25 | 1.182–1.305 |
| No. 1-72 (1.854) | 1.55 | 1.474–1.612 |
| No. 2-64 (2.184) | 1.85 | 1.756–1.912 |
| No. 3-56 (2.515) | 2.10 | 2.025–2.197 |
| No. 4-48 (2.845) | 2.40 | 2.271–2.458 |
| No. 5-44 (3.175) | 2.70 | 2.551–2.740 |
| No. 6-40 (3.505) | 2.90 | 2.820–3.022 |
| No. 8-36 (4.166) | 3.50 | 3.404–3.606 |
| No. 10-32 (4.826) | 4.10 | 3.963–4.165 |
| 1/4-28 | 5.50 | 5.360–5.588 |
| 5/16-24 | 6.90 | 6.782–7.035 |
| 3/8-24 | 8.50 | 8.382–8.636 |
| 7/16-20 | 9.90 | 9.729–10.033 |
| 1/2-20 | 11.50 | 11.329–11.607 |
| 9/16-18 | 12.90 | 12.751–13.081 |
| 5/8-18 | 14.50 | 14.351–14.681 |
| 3/4-16 | 17.50 | 17.323–17.678 |
| 7/8-14 | 20.50 | 20.270–20.675 |
| 1-12 | 23.20 | 23.114–23.571 |
| 1-1/8-12 | 26.50 | 26.289–26.746 |
| 1-1/4-12 | 29.50 | 29.464–29.921 |
| 1-3/8-12 | 32.80 | 32.639–33.096 |
| 1-1/2-12 | 36.00 | 35.814–36.271 |
Metric fine threads
Show the metric fine table (71 sizes)
| Thread | Drill, mm | Hole limits, mm |
|---|---|---|
| M1.0×0.2 | 0.80 | 0.783–0.821 |
| M1.1×0.2 | 0.90 | 0.883–0.921 |
| M1.2×0.2 | 1.00 | 0.983–1.021 |
| M1.4×0.2 | 1.20 | 1.183–1.221 |
| M1.6×0.2 | 1.40 | 1.383–1.421 |
| M1.8×0.2 | 1.60 | 1.583–1.621 |
| M2.0×0.25 | 1.75 | 1.729–1.785 |
| M2.2×0.25 | 1.95 | 1.929–1.985 |
| M2.5×0.35 | 2.20 | 2.121–2.221 |
| M3.0×0.35 | 2.70 | 2.621–2.721 |
| M3.5×0.35 | 3.20 | 3.121–3.221 |
| M4.0×0.5 | 3.50 | 3.459–3.599 |
| M4.5×0.5 | 4.00 | 3.959–4.099 |
| M5.0×0.5 | 4.50 | 4.459–4.599 |
| M5.5×0.5 | 5.00 | 4.959–5.099 |
| M6.0×0.75 | 5.30 | 5.188–5.378 |
| M7.0×0.75 | 6.30 | 6.188–6.378 |
| M8.0×1.0 | 7.00 | 6.917–7.153 |
| M8.0×0.75 | 7.30 | 7.188–7.378 |
| M9.0×1.0 | 8.00 | 7.917–8.153 |
| M9.0×0.75 | 8.30 | 8.188–8.378 |
| M10×1.25 | 8.80 | 8.647–8.912 |
| M10×1.0 | 9.00 | 8.917–9.153 |
| M10×0.75 | 9.30 | 9.188–9.378 |
| M11×1.0 | 10.00 | 9.917–10.153 |
| M11×0.75 | 10.30 | 10.188–10.378 |
| M12×1.5 | 10.50 | 10.376–10.676 |
| M12×1.25 | 10.80 | 10.647–10.912 |
| M12×1.0 | 11.00 | 10.917–11.153 |
| M14×1.5 | 12.50 | 12.376–12.676 |
| M14×1.0 | 13.00 | 12.917–13.153 |
| M15×1.5 | 13.50 | 13.376–13.676 |
| M15×1.0 | 14.00 | 13.917–14.153 |
| M16×1.5 | 14.50 | 14.376–14.676 |
| M16×1.0 | 15.00 | 14.917–15.153 |
| M17×1.0 | 16.00 | 15.917–16.153 |
| M18×2.0 | 16.00 | 15.835–16.21 |
| M18×1.5 | 16.50 | 16.376–16.676 |
| M18×1.0 | 17.00 | 16.917–17.153 |
| M20×2.0 | 18.00 | 17.835–18.21 |
| M20×1.5 | 18.50 | 18.376–18.676 |
| M20×1.0 | 19.00 | 18.917–19.153 |
| M22×2.0 | 20.00 | 19.835–20.21 |
| M22×1.5 | 20.50 | 20.376–20.676 |
| M22×1.0 | 21.00 | 20.917–21.153 |
| M24×2.0 | 22.00 | 21.835–22.21 |
| M24×1.5 | 22.50 | 22.376–22.676 |
| M24×1.0 | 23.00 | 22.917–23.153 |
| M25×2.0 | 23.00 | 22.835–23.21 |
| M25×1.5 | 23.50 | 23.376–23.676 |
| M25×1.0 | 24.00 | 23.917–24.153 |
| M26×1.5 | 24.50 | 24.376–24.676 |
| M27×2.0 | 25.00 | 24.835–25.21 |
| M27×1.5 | 25.50 | 25.376–25.676 |
| M27×1.0 | 26.00 | 25.917–26.153 |
| M28×2.0 | 26.00 | 25.835–26.21 |
| M28×1.5 | 26.50 | 26.376–26.676 |
| M28×1.0 | 27.00 | 26.917–27.153 |
| M30×3.0 | 27.00 | 26.752–27.252 |
| M30×2.0 | 28.00 | 27.835–28.21 |
| M30×1.5 | 28.50 | 28.376–28.676 |
| M30×1.0 | 29.00 | 28.917–29.153 |
| M32×2.0 | 30.00 | 29.835–30.21 |
| M32×1.5 | 30.50 | 30.376–30.676 |
| M33×3.0 | 30.00 | 29.752–30.252 |
| M33×2.0 | 31.00 | 30.835–31.21 |
| M33×1.5 | 31.50 | 31.376–31.676 |
| M35×1.5 | 33.50 | 33.376–33.676 |
| M36×3.0 | 33.00 | 32.752–33.252 |
| M36×2.0 | 34.00 | 33.835–34.21 |
| M36×1.5 | 34.50 | 34.376–34.676 |
Pipe threads (G, PT, NPT) and Whitworth are in the same catalog chapter: catalog chapter 07, Technical data (PDF).
Tap or thread mill?
The drill size is the same for both. A thread mill is usually the better choice when:
- the part is valuable and a broken tap would scrap it
- the material is hard, tough or gummy, such as hardened steel, titanium or stainless steel
- you need several thread sizes at the same pitch from one tool
- the thread is large, where a tap needs high torque
- the thread runs close to the bottom of a blind hole
A tap is usually quicker for small, standard threads in free-cutting material at high volumes. The full comparison is in Thread milling vs tapping.
Our thread mills
Solid carbide thread mills for metric coarse threads M0.8–M33, fine threads to M48 and, by pitch, sizes to M80, plus UN, NPT/NPTF, BSP/BSPT, TR, ACME and PG threads. 3-in-1 drill and thread mills (M6–M12 in the catalog) drill the pre-hole and cut the thread with one tool. Other sizes are made to your drawing.
Need a size that isn’t listed, or a thread mill for it?
Send us:
- The thread size and class, and whether it is a through or blind hole
- Workpiece material and hardness
- Thread depth, and the machine and holder you will use
- Quantity per size